Explore our flagship heavy-duty storage configurations engineered for maximum space utilization and seamless material handling.

Mbarara, as the official primary city of Western Uganda and the strategic nerve center of the Ankole sub-region, is experiencing an unprecedented structural transformation. Positioned along the vital Trans-African Highway corridor connecting Kampala to Rwanda (via Gatuna and Kagitumba), the Democratic Republic of Congo (via the Bunagana and Kasindi borders), and northern Tanzania, Mbarara has rapidly outgrown traditional warehousing architectures. The local economic landscape—historically anchored by commercial livestock farming and dairy production—has evolved into a complex, multi-tiered industrial hub encompassing large-scale milk processing factories, grain milling complexes, beverage bottling plants, pharmaceutical distribution centers, and regional fast-moving consumer goods (FMCG) logistics depots.
This dynamic commercial acceleration presents a critical operational challenge for warehouse managers and logistics operators across Mbarara: maximizing vertical storage footprint while strictly maintaining inventory integrity and operational safety. Traditional selective pallet racking, while offering 100% immediate accessibility, demands multiple access aisles that consume upwards of 50% to 60% of total warehouse floor area. In rapid-growth economic zones like Mbarara’s Biharwe industrial park, Rayon Village, and along the Mbarara-Kabale highway, commercial land values and warehouse construction costs have surged. Storage managers can no longer afford wasted aisle space when storing high-volume, uniform SKUs such as UHT milk cartons, processed grain sacks, packaged beverages, and cold-stored agricultural produce.
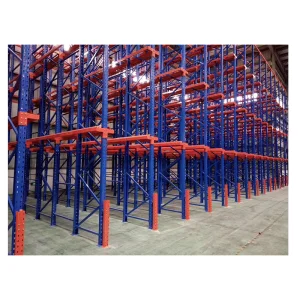
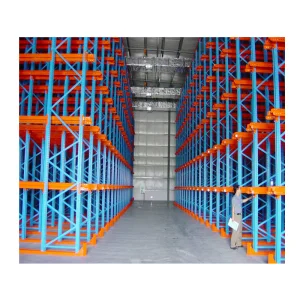
By eliminating forklift working aisles between storage bays, Drive-In Pallet Racks provide a high-density solution that increases floor area utilization by 75% to 85% compared to standard pallet racking systems. Forklifts drive directly into the structural lanes to deposit or retrieve pallets resting on continuous support rails. This architectural blueprint allows enterprise operators in Mbarara to double their effective pallet capacity within existing warehouse footprints without incurring expensive facility expansion costs.
Furthermore, Western Uganda’s cold chain supply infrastructure relies heavily on energy-intensive refrigerated storage environments (cold rooms operating from -18°C to +4°C). The electrical operational cost per cubic meter in cold storage facility management demands absolute density. Implementing customized Drive-In racking within cold storage facilities across Mbarara drastically reduces thermal dissipation per pallet position, yielding substantial long-term operational savings for dairy processing leaders and export-oriented food producers.
Empowering Mbarara’s industrial infrastructure through world-class engineering, rigorous quality controls, and proven international export reliability.
Every rack system crafted for our Mbarara client base undergoes stringent structural testing. Our quality control division consists of 45 professional inspectors performing automated ultrasonic testing, raw material tension evaluations (Q235B & Q355B high-grade steel), electrostatic powder coating thickness verification, and beam load deflection checks.
Supported by 85 experienced structural engineers, Maobang provides comprehensive warehouse spatial design, AutoCAD floor plan rendering, 3D stress modeling, seismic calculation, and load analysis tailored specifically to Mbarara's local soil loading capacities and warehouse roof clearance heights.
A deep technical analysis of components, load distribution mechanics, and operational safety standards.
Drive-In racking systems operate on the First-In, Last-Out (FILO) storage principle, making them uniquely suited for bulk goods, homogeneous inventory, and high-volume SKU rotation. Alternatively, when configured as a Drive-Through system (accessible from both front and rear entry points), the system can support First-In, First-Out (FIFO) stock management protocols.
Unlike standard selective rack structures that rely on transverse horizontal support beams underneath each pallet, Drive-In systems utilize heavy-duty cantilever support arms anchored to vertical upright frames. The pallets rest directly on continuous cold-formed steel guide rails that run the full depth of the lane.
| Structural Element | Engineering Specification | Operational Function in Mbarara Installations |
|---|---|---|
| Upright Frames | High-tensile cold-rolled steel (Q235B / Q355B grade); pitch adjustment 50mm / 75mm | Transfers cumulative vertical loading safely to the warehouse concrete slab. |
| Corbel / Support Arms | Heavy-gauge stamped steel cantilever brackets (Single & Double side) | Secures horizontal support rails to upright posts with high torsional rigidity. |
| Pallet Support Rails | Custom structural steel profiles (C-channel or rolled top flange) | Provides smooth, low-friction support channels for loaded wood, metal, or plastic pallets. |
| Top & Back Bracing | Diagonal and horizontal structural bracing lattice | Eliminates lateral sway and stabilizes high-bay bays (elevations up to 12 meters). |
| Ground Floor Guide Rails | Floor-anchored steel angle iron or structural C-channel tracking | Guides forklift drivers inside narrow lanes, preventing accidental upright column impacts. |
| Column Protectors | Heavy-duty floor-mounted rubber/steel safety wraps with yellow epoxy finish | Absorbs dynamic impacts from forklift chassis at lane entrances. |
When engineering Drive-In racks for enterprise operations in Mbarara, Maobang’s R&D division calculates critical structural metrics including frame bucking resistance, dynamic impact tolerance, and live loading deflection ratios in according with FEM 10.2.02 and ANSI/RMI MH16.1 international standards. Pallet positions are rated for loads ranging from 500 kg to over 1,500 kg per pallet, with overall bay load capacities exceeding 15,000 kg depending on system depth and ceiling height.
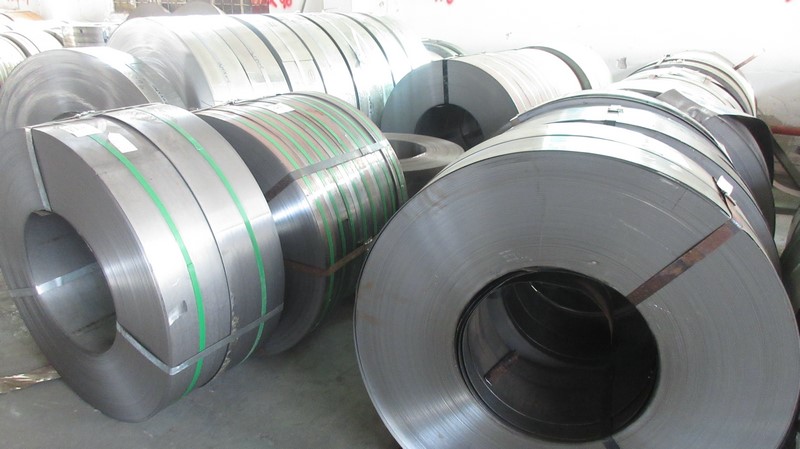
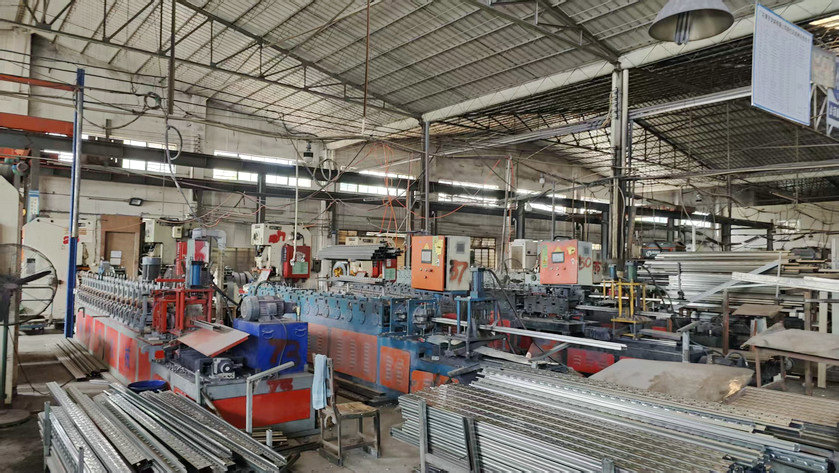
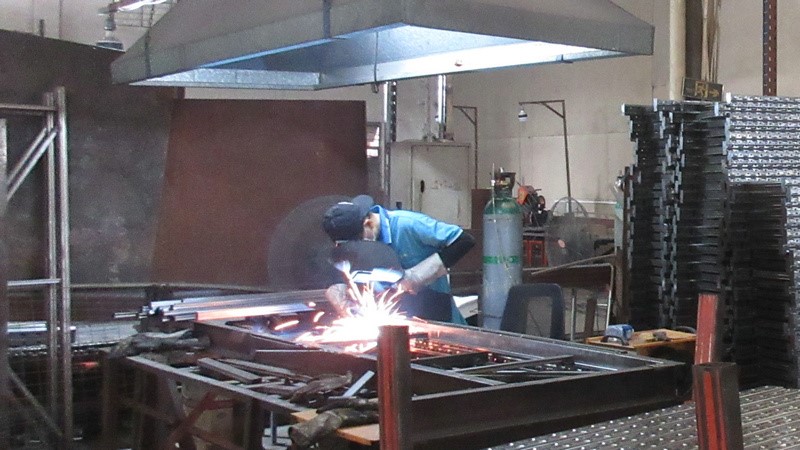
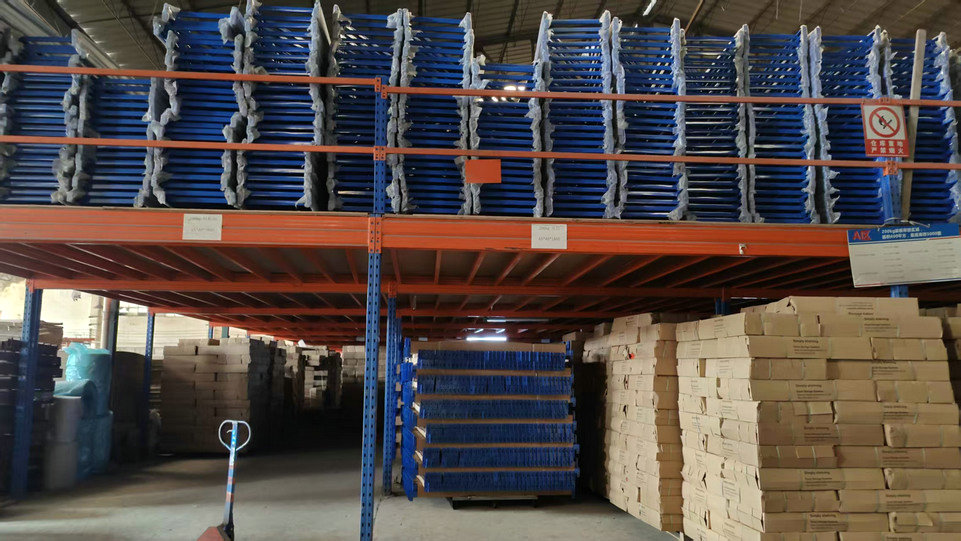
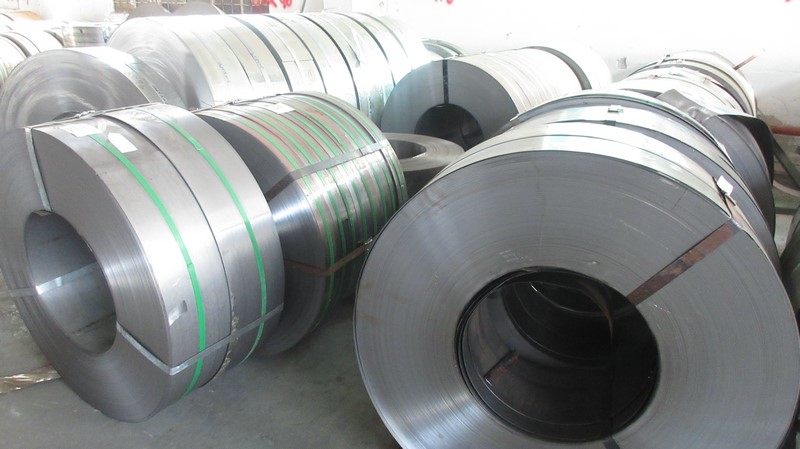
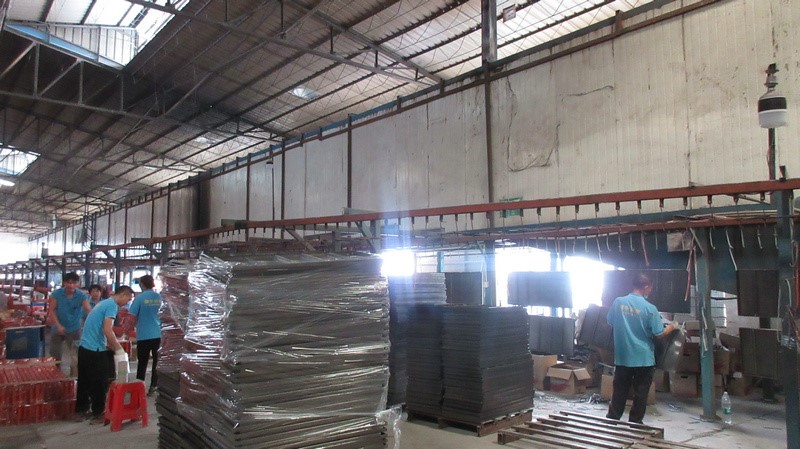
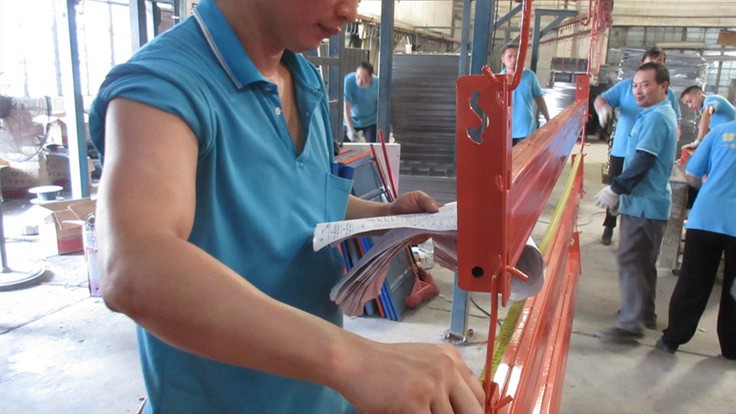
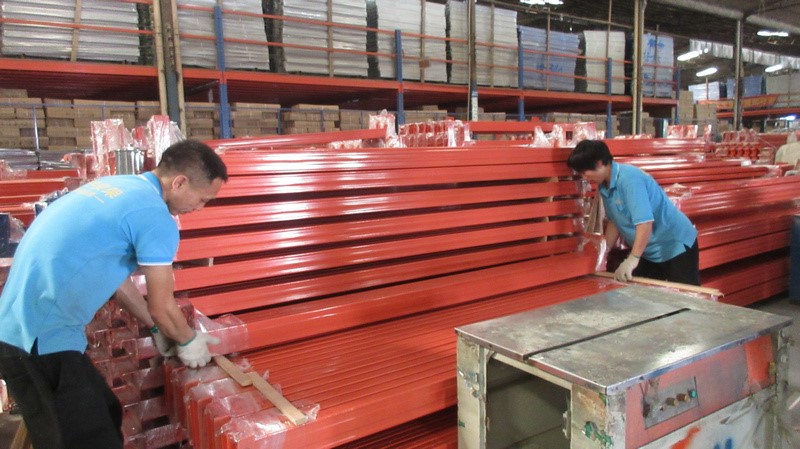
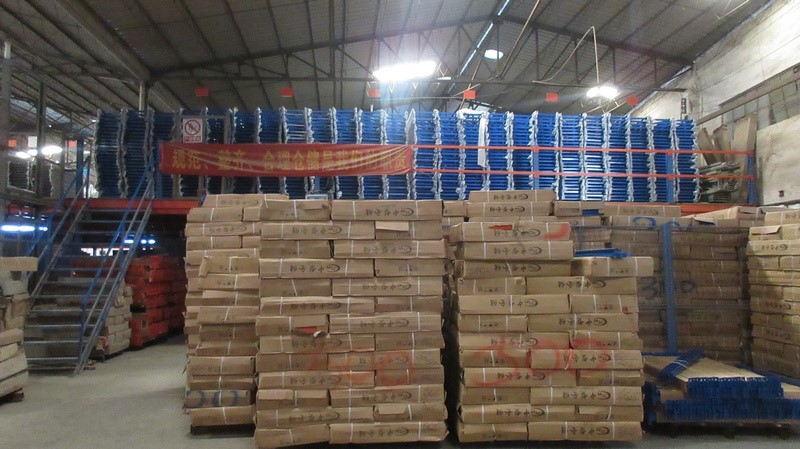
From raw steel coil processing to automated powder coating—exploring our state-of-the-art production workflow.
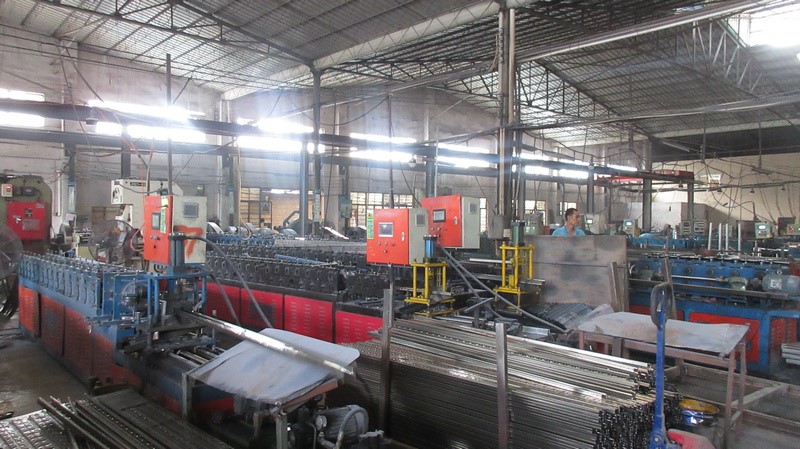
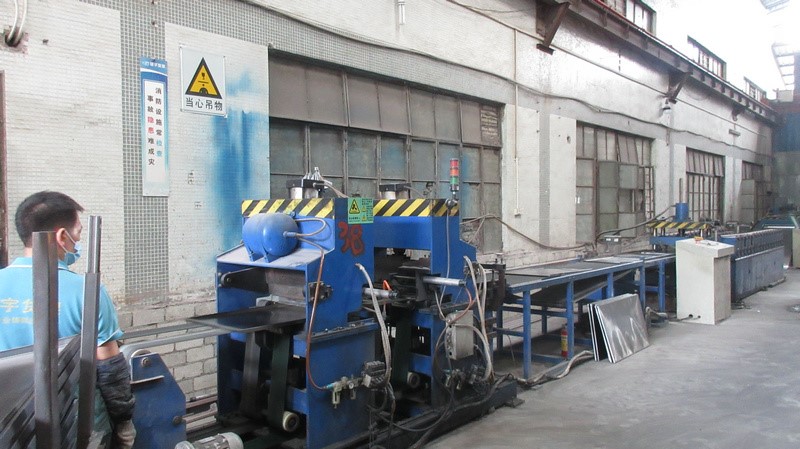
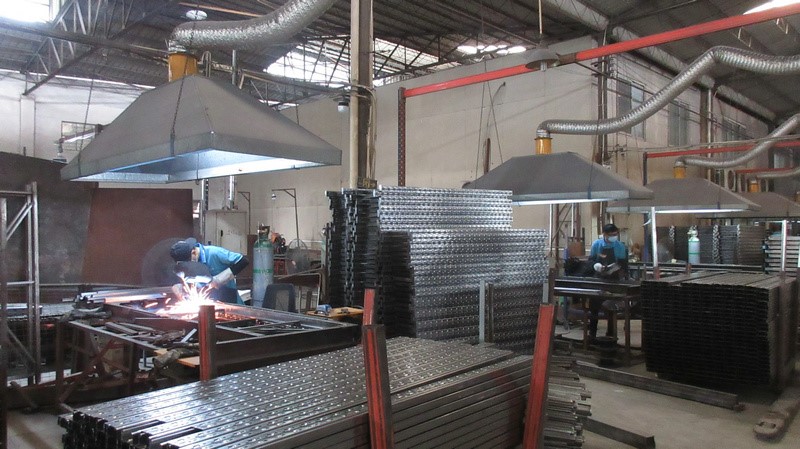
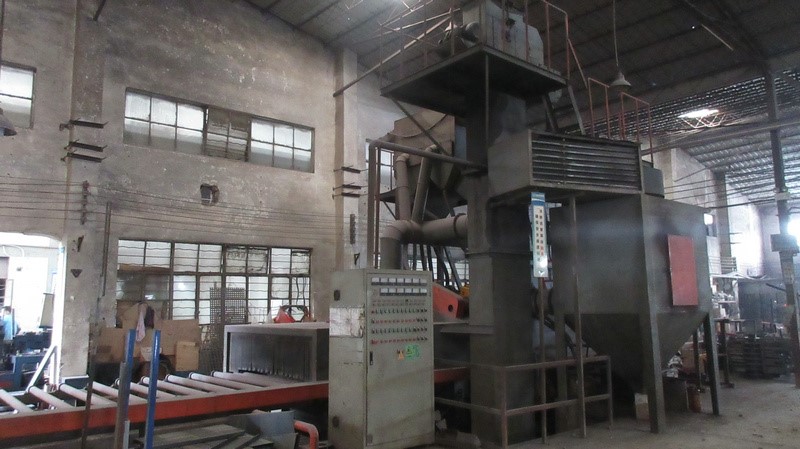
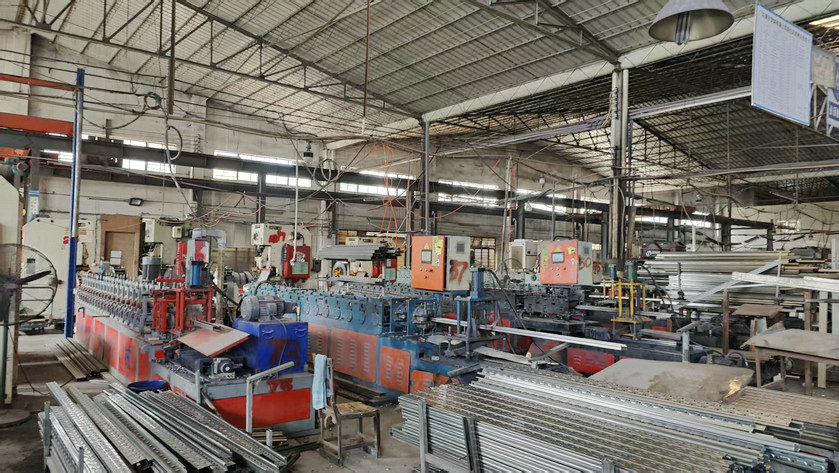
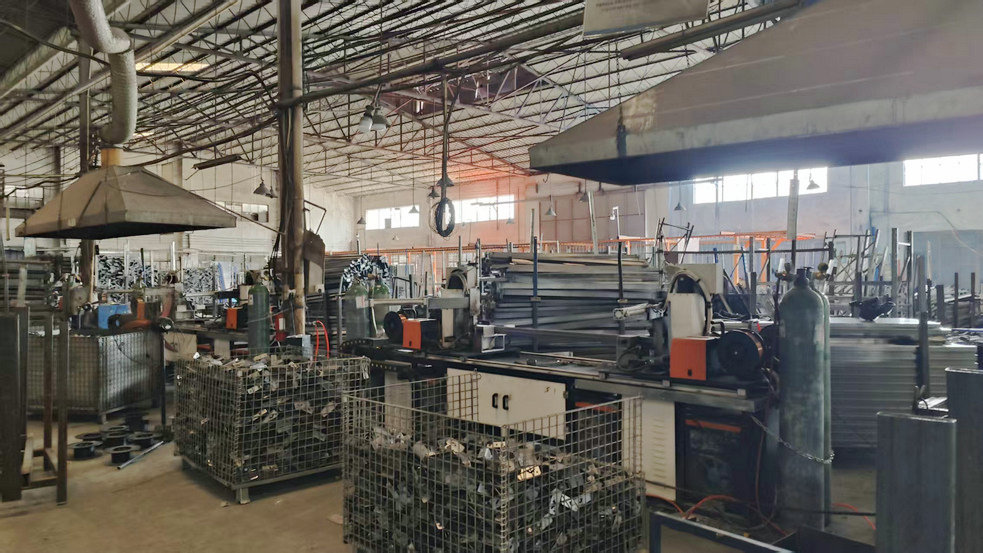
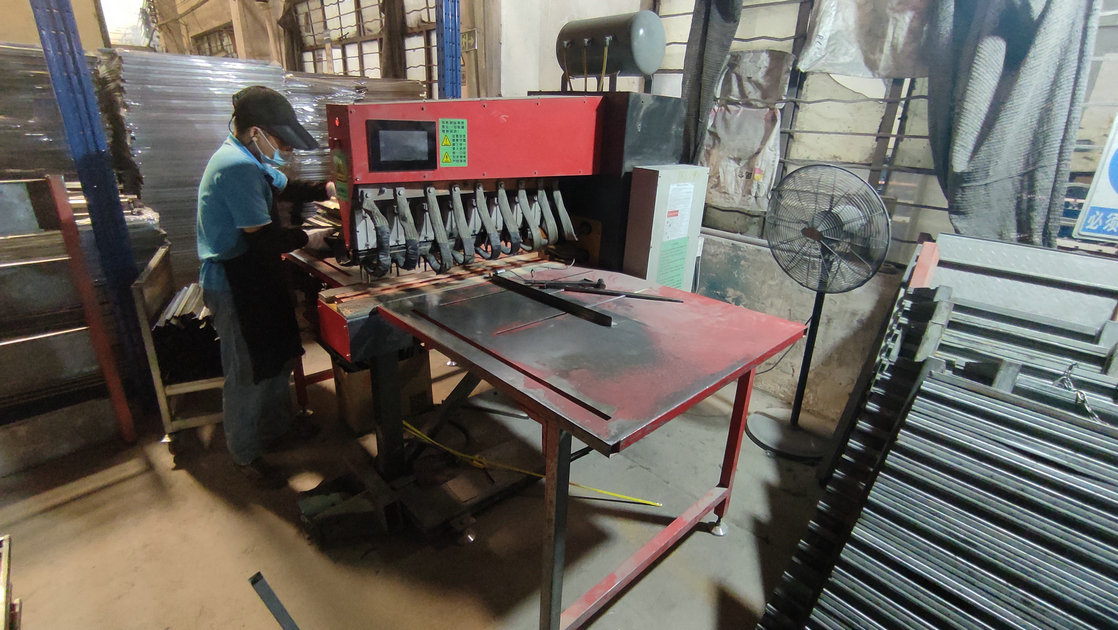
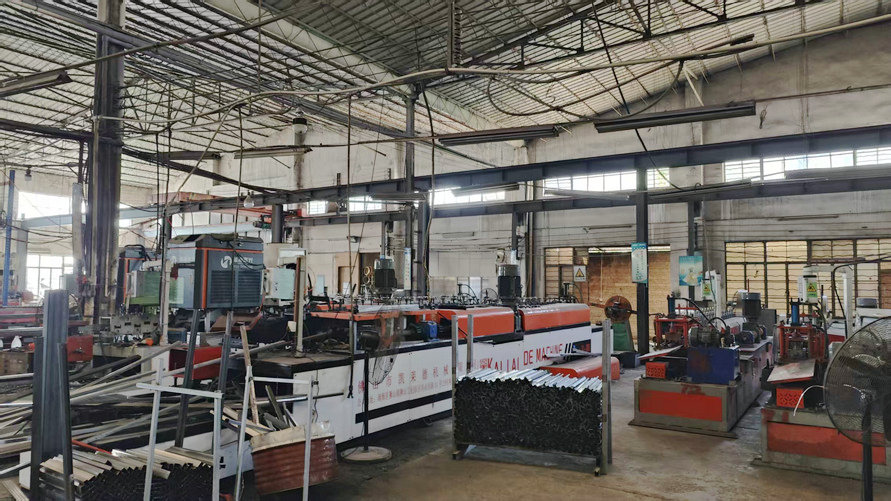
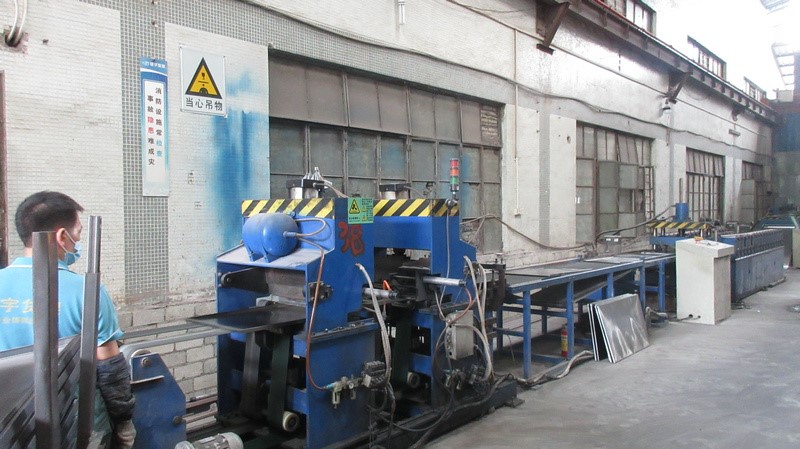
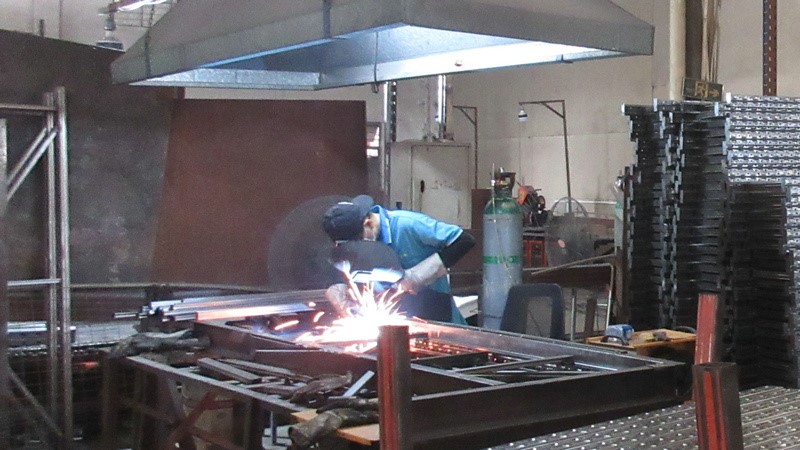
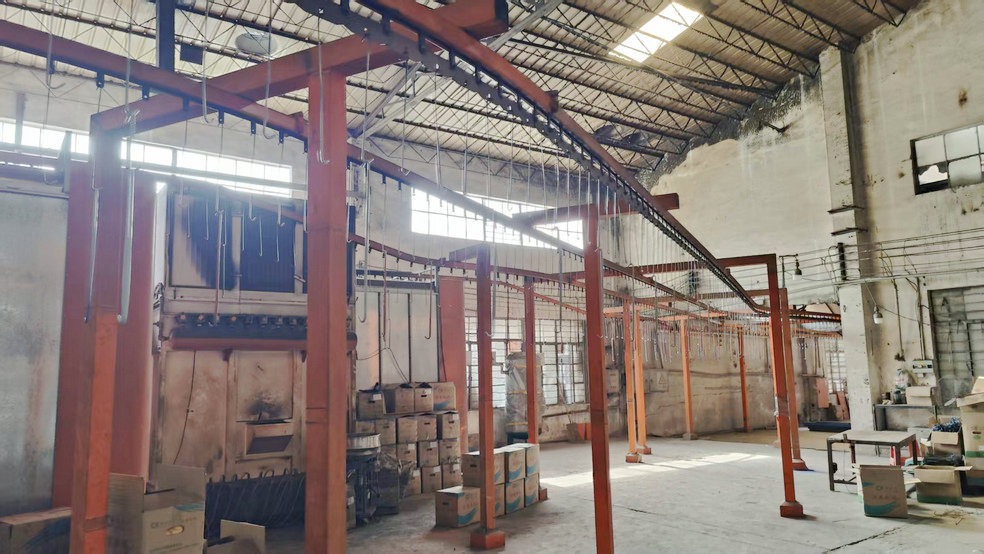
Integrating smart technologies, IoT sensors, and shuttle automation with high-density racking.
As Western Uganda accelerates its regional integration within the East African Community (EAC) market, logistics infrastructure in Mbarara must adapt to next-generation warehouse management demands. The transition from legacy manual storage to semi-automated and fully automated high-density ecosystems is already underway.
While traditional Drive-In systems require forklift operators to drive inside racking channels, modern hybrid systems utilize automated radio shuttle carts. The shuttle car travels along internal rails under remote command, placing and retrieving pallets at high speeds while the forklift remains safely outside the aisle. For enterprise warehouses in Mbarara handling high-volume milk powder, grain bags, or bottled mineral water, upgrading to shuttle-compatible drive-in frames dramatically boosts throughput speeds while eliminating collision risks with upright columns.
Mbarara's equatorial highland climate features distinct rainy seasons and high ambient humidity levels. Maobang implements advanced thermosetting epoxy-polyester powder coatings subjected to 13-stage pre-treatment chemical washing and high-temperature curing. This provides exceptional corrosion protection, scratch resistance, and hygienic surfaces that comply with international food-grade logistics standards.
Installing high-bay rack systems (exceeding 8 to 10 meters in height) in Mbarara requires strict structural engineering compliance. Maobang provides detailed concrete slab load requirements (such as minimum C25/C30 concrete grade with structural steel rebar mesh) and supplies dynamic anchor bolt calculations to withstand seismic tremors associated with the East African Rift Valley network.
Explore our complete range of customized racking units engineered for factories, logistics centers, and retail outlets in Mbarara.

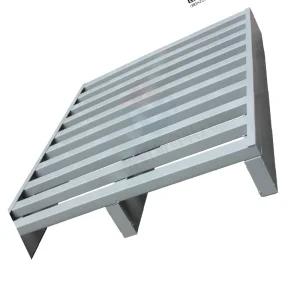
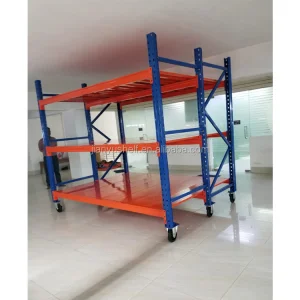

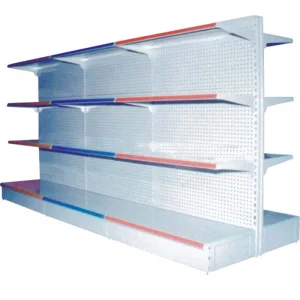
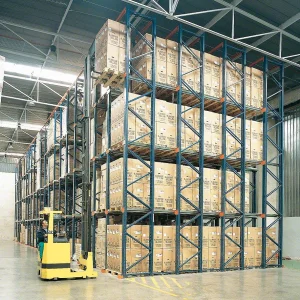
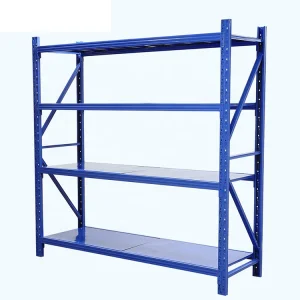
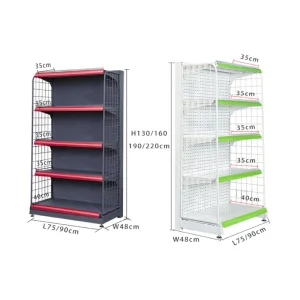
Modular multi-tier systems, selective beam racks, and steel decking customized for Mbarara enterprise facilities.
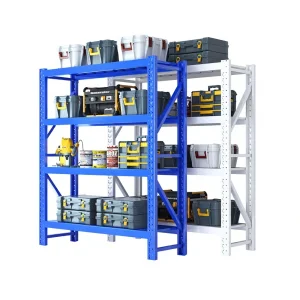
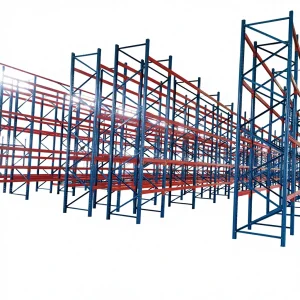


Comprehensive answers from our chief engineering team regarding design, installation, shipping, and safety maintenance.
Drive-In racking is specifically designed for high-density storage of uniform, high-volume products. In Mbarara's thriving dairy and agro-processing sector, companies typically handle large batches of single-SKU goods (such as long-life milk powder bags, butter blocks, or packaged grains). Drive-In racking maximizes cubic warehouse density by up to 85% by eliminating intermediate forklift aisles, drastically reducing the cost per pallet position, especially within climate-controlled cold storage facilities.
FILO (First-In, Last-Out) Drive-In systems utilize a single entry/exit aisle per storage lane. Forklifts load and unload from the same side, making the last pallet stored the first one to be retrieved. FIFO (First-In, First-Out / Drive-Through systems) feature separate entry and exit aisles on opposite sides of the rack structure. Pallets are loaded from the rear and retrieved from the front, ensuring strict stock rotation for date-sensitive perishables.
Because forklifts physically operate inside the racking channels, structural clearances are critical. We recommend installing heavy-duty floor-anchored steel angle guide rails along the lane floor. These guide rails align the forklift chassis automatically, preventing collision damage to upright posts and cantilever support arms. A minimum lateral safety clearance of 75mm to 100mm between the forklift mast/load and the rack posts is engineered into every Maobang design.
Maobang has over 7 years of direct international export experience serving East Africa. Orders are securely packaged in steel-strapped bundles and protective bubble film, shipped via 40ft High Cube containers to the Port of Mombasa (Kenya) or Dar es Salaam (Tanzania), and transported via overland freight directly to your warehouse location in Mbarara. We provide comprehensive AutoCAD installation drawings, step-by-step video manuals, and can dispatch structural engineering advisors for on-site installation supervision upon request.
Yes. Maobang's 85-member R&D engineering department customizes beam levels, upright depth, corbel arm overhang, and rail widths to accommodate any pallet specification, including Euro pallets (800x1200mm), Industrial pallets (1000x1200mm / 1200x1200mm), heavy-duty steel pallets, and custom agricultural wooden crates widely used across Western Uganda.
Partner with Guangdong Maobang Storage Equipment Co., Ltd. for turnkey structural engineering, factory-direct wholesale pricing, and custom high-density drive-in racking solutions.
Send Inquiry Now Maobang Storage